


Solution
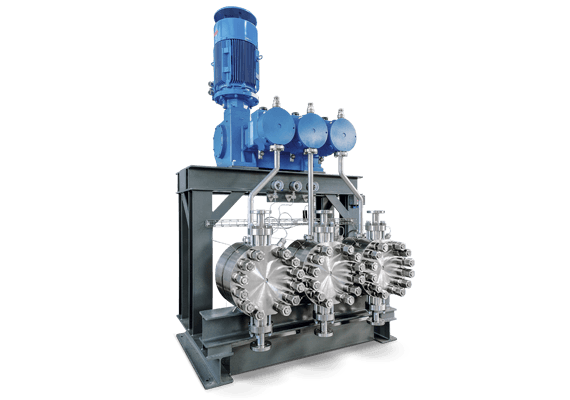
Remote-head metering pumps are used for coal injection because they offer the following benefits:
- Reliable operation thanks to spatial separation of the valve head and displacement system
- A falling hydraulic connecting line (if necessary, with cooling jacket) prevents sedimentation in the fluid chamber.
- A flushing pump keeps slurry particles away from the plunger seal.
- The hermetic seal of our pump technology ensures reliable conveyance of potentially hazardous substances, which are required for the chemical reaction (e.g. hydrocyanic acid or hydrogen sulfide).
- Any gas bubbles that have accumulated are carried away through the gas removal valve and into the main line by a small discharge flow.
Background
How and why is coal refined?
Coal refinement enables the production of various successor products from coal. Raw lignite cannot be used until it has been processed in a coal refinery, for example, by being made into briquettes, pulverized lignite or fluidized-bed lignite.
One kind of coal refinement is coal liquefaction, which uses the Fischer-Tropsch method, among others. For this, the coal must first be gasified at temperatures over 1000 °C while steam and air or oxygen are fed. The resulting synthetic gas is then cooled. During this process, phenol, liquid ammonia, carbon dioxide, hydrogen sulfide, hydrocyanic acid and organic components are removed from the gas. Then the synthetic gas is converted into hydrocarbons (such as paraffins and alcohols) in a heterogeneous catalytic reaction.
A Fischer-Tropsch synthesis results in various end products such as synthetic gasoline, diesel, heating oil and diverse raw materials for the chemical industry.


